- Home
- Products
- Company
- Case Study
- News
- Contact Us
Leave Your Message
High-precision medical grade solutions engineered for reliability, safety, and strict regulatory compliance.
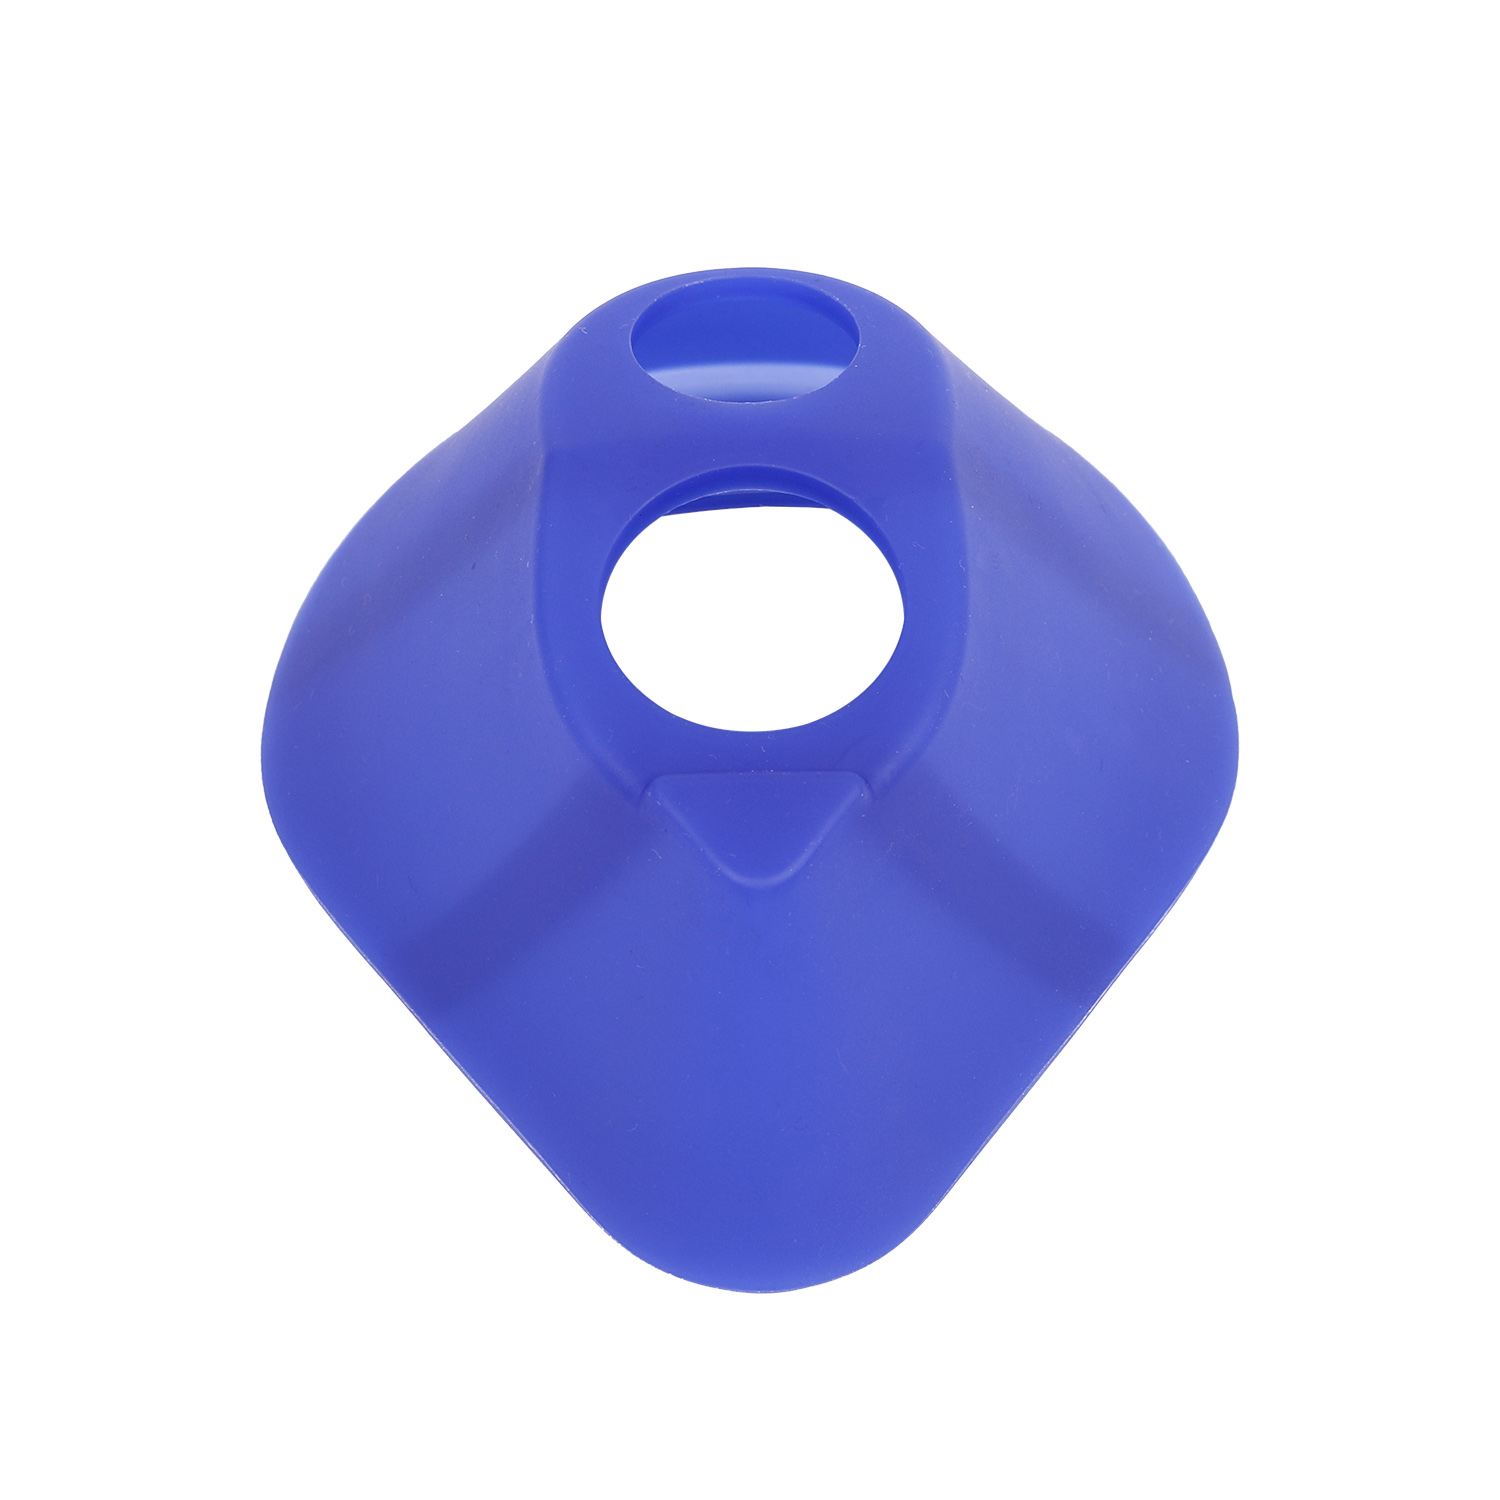
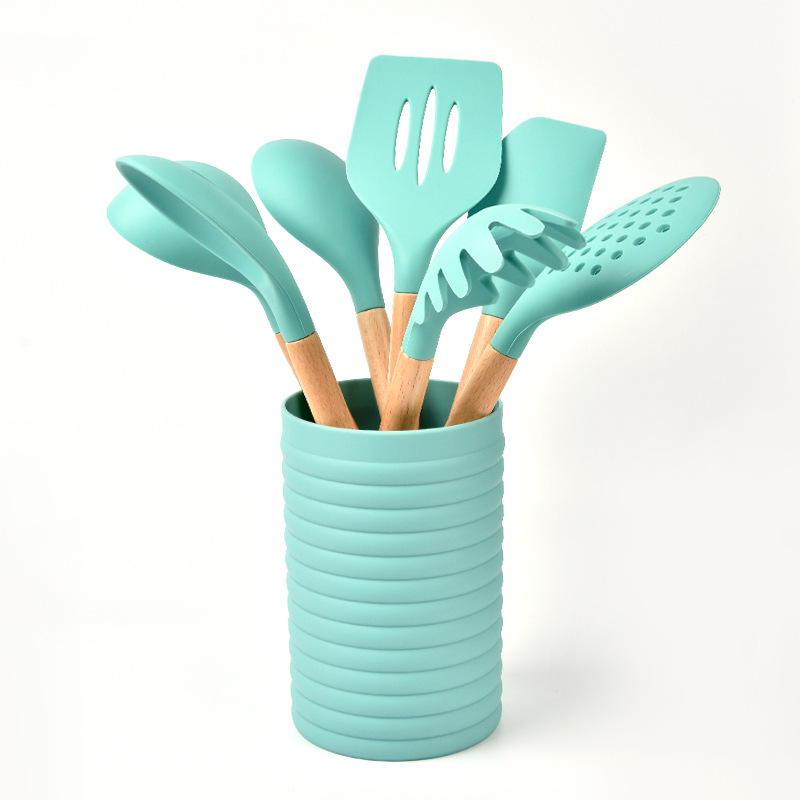
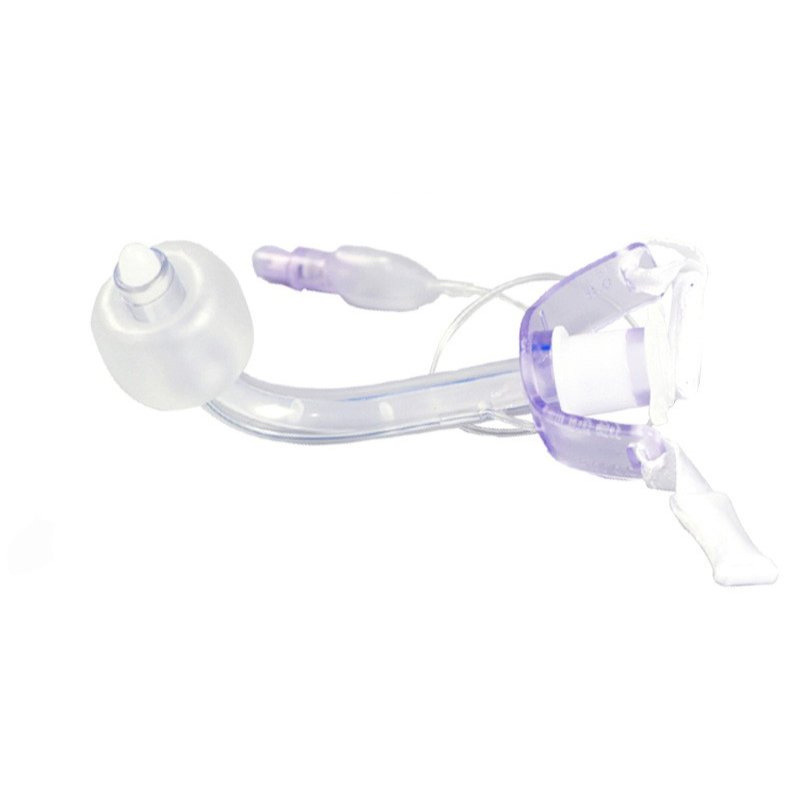
In the highly regulated medical device sector, fluid management, containment, and delivery systems demand materials of the highest purity and performance. The silicone bottle for medical device manufacturers has transitioned from a specialty component to an industry standard. Liquid Silicone Rubber (LSR) and high-consistency silicone (HCR) are favored for their biocompatibility, flexibility, durability, and resistance to extreme temperatures and chemical agents.
Unlike traditional glass or rigid plastics, medical-grade silicone does not leach harmful chemicals, crack under impact, or degrade during rigorous sterilization cycles. This makes silicone bottles ideal for applications ranging from wound drainage systems and enteral feeding reservoirs to drug delivery pumps and diagnostic fluid containers.
Medical OEMs are increasingly integrating sensors and microfluidic channels directly into silicone bottles, turning simple containment into active, smart delivery systems.
Silicone bottles are widely utilized as vacuum reservoirs in surgical wound drainage. Their elastic recovery properties allow them to maintain constant negative pressure, gently drawing fluids away from the surgical site. The transparency of medical silicone allows clinical staff to monitor fluid color and volume accurately, while its soft texture ensures patient comfort during portable therapies.
For neonatal and pediatric care, silicone bottles provide a completely BPA-free, phthalate-free, and latex-free solution. Because silicone mimics natural tissue softness, it is widely used in specialized feeding systems for infants with cleft palates or suction difficulties. These bottles can withstand repeated autoclaving without losing their structural integrity or mechanical properties.
In ambulatory infusion pumps, elastomeric silicone reservoirs (often designed as collapsible bottles or balloons) act as the primary driving force for drug delivery. The constant elastomeric pressure of the silicone walls dispenses medication at a controlled rate without the need for batteries or external power. This requires extreme wall-thickness precision during the molding process.
Diagnostics and laboratory automation require chemically inert containers to store sensitive reagents. Medical-grade silicone bottles prevent absorption of active ingredients and maintain sample integrity. Furthermore, their ability to withstand cryogenic temperatures makes them ideal for biobanking and long-term storage of biological agents.
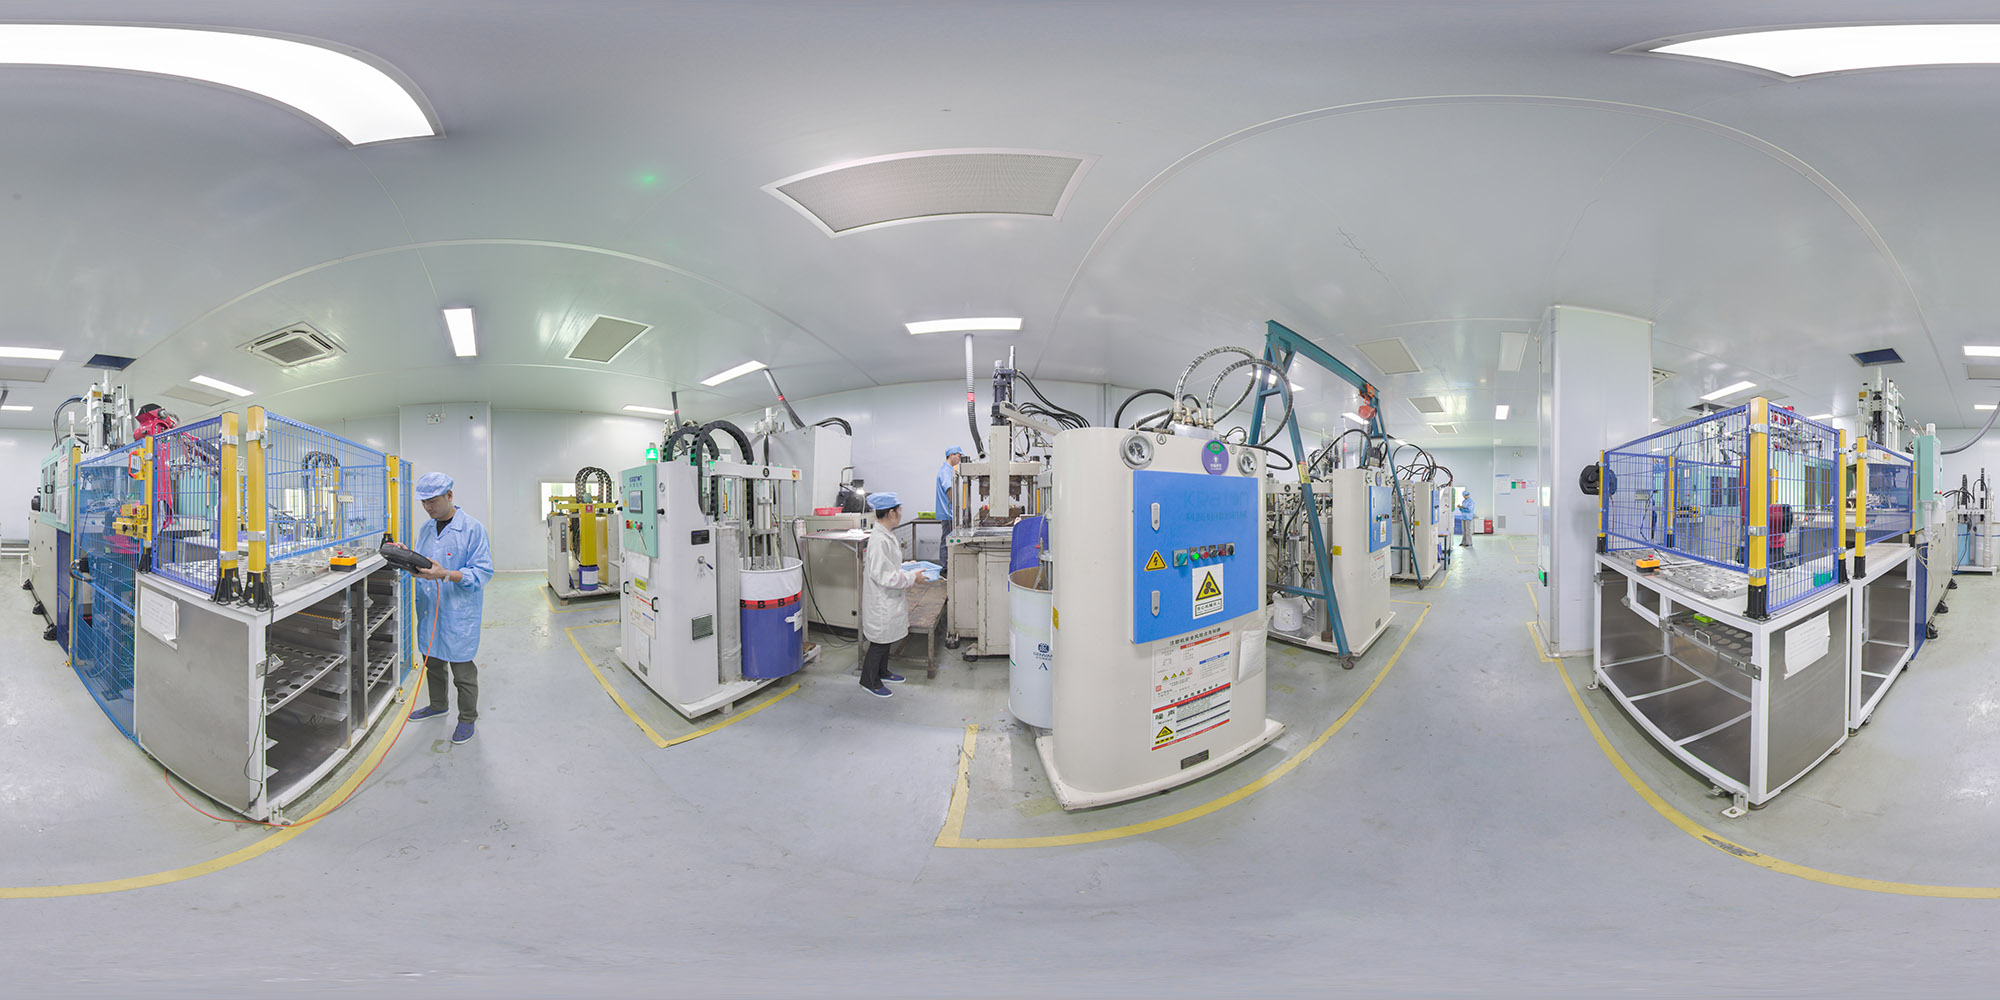
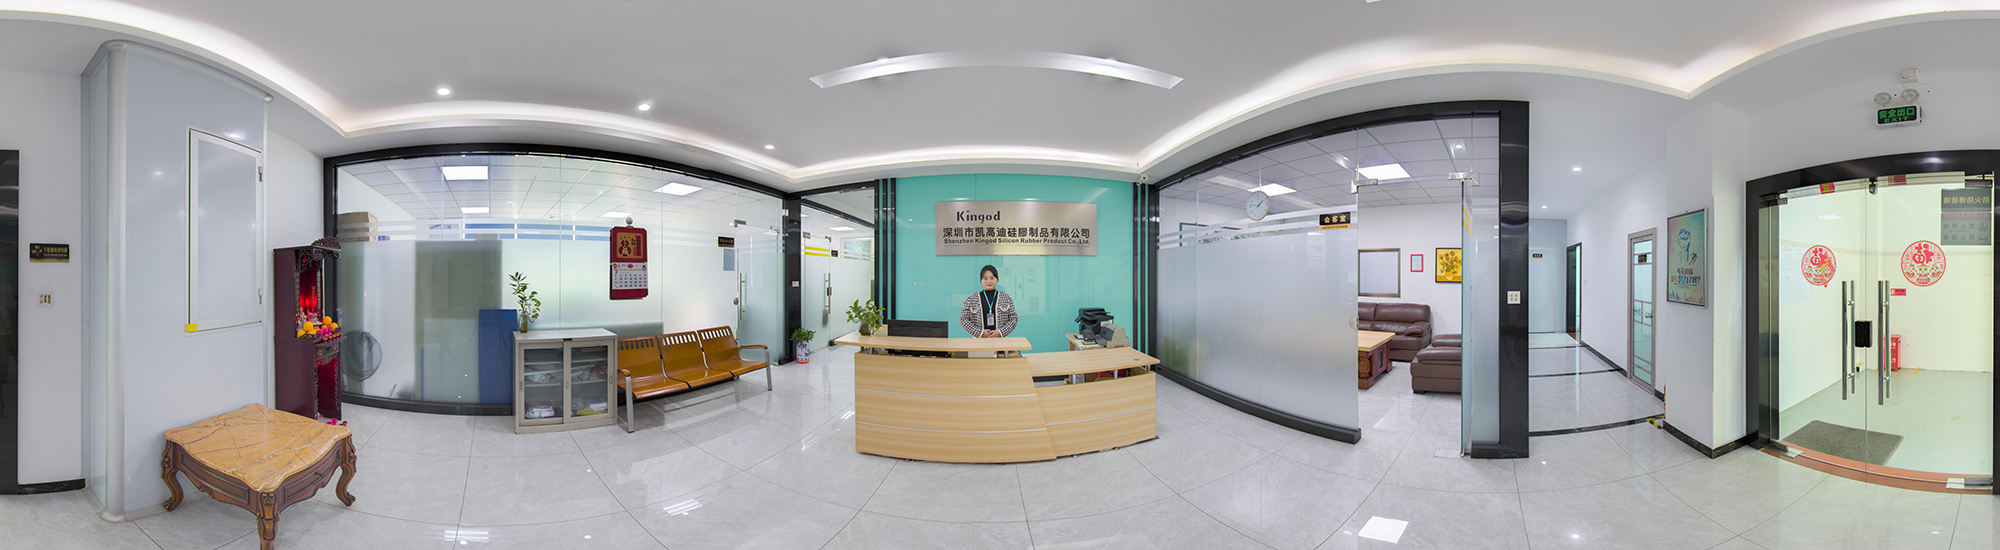
Kingod Silicone Products Co., Ltd. is a custom silicone manufacturer established in 2006. We specialize in precision silicone products and use automated production equipment to improve consistency, and product quality for global customers.
Since its establishment, Kingod has focused on advancing silicone processing technologies and expanding production capabilities. Headquartered in Shenzhen, Guangdong Province, the company operates from a modern factory spanning over 3,000 square meters, equipped with state-of-the-art machinery and a skilled workforce. Over the years, Kingod has built a reputation for excellence through continuous technological investment and strict quality management.
For medical device manufacturers, selecting the right raw material is a matter of patient safety and regulatory approval. Medical-grade silicones must pass rigorous biocompatibility testing, including ISO 10993 (cytotoxicity, sensitization, irritation, and systemic toxicity) and USP Class VI standards. The material must remain inert when in contact with human tissue, blood, or pharmaceutical formulations.
LSR is processed via injection molding, offering high precision, short cycle times, and complex geometry capabilities. It is ideal for high-volume medical bottles requiring tight tolerances, integrated valves, or multi-material overmolding. Its closed-loop processing ensures minimal risk of environmental contamination.
HCR (often processed via compression molding or extrusion) features high green strength and excellent mechanical properties. It is commonly selected for custom medical bottles with thicker walls or simple configurations where cost-efficiency and robust tensile strength are prioritized.
Sterilization compatibility is another major advantage of silicone. Medical silicone bottles can be sterilized using several standard clinical methods without undergoing physical deformation or chemical degradation:
We specialize in Liquid Silicone Rubber (LSR) and High-Temperature Vulcanized (HTV) silicone Compression molding, offering end-to-end custom manufacturing services. Our product portfolio covers a wide spectrum of industries, including:
Food-grade silicone items such as nipples, pacifiers, and feeding utensils.
Medical-grade silicone components for devices, seals.
Heat-resistant, non-toxic silicone kitchen tools, bakeware, and home accessories.
Durable silicone seals, gaskets, connectors, and protective components.
A key innovation in the production of a silicone bottle for medical device manufacturers is multi-material overmolding. This process allows liquid silicone rubber to be chemically or mechanically bonded directly to rigid plastic substrates (such as polycarbonate, PEEK, or polysulfone) or metal components without the use of primers or adhesives.
This technology is critical for medical devices because it eliminates micro-gaps where bacteria can accumulate, creating a completely sterile, leak-proof barrier. For example, a medical silicone bottle can be molded directly onto a rigid plastic threaded neck or fluid connector, simplifying the device assembly process, reducing the bill of materials (BOM), and enhancing overall device reliability.
Using state-of-the-art CNC machining and cold runner systems, we maintain tolerances as low as ±0.05mm, ensuring consistent wall thickness and predictable elastomeric behavior.
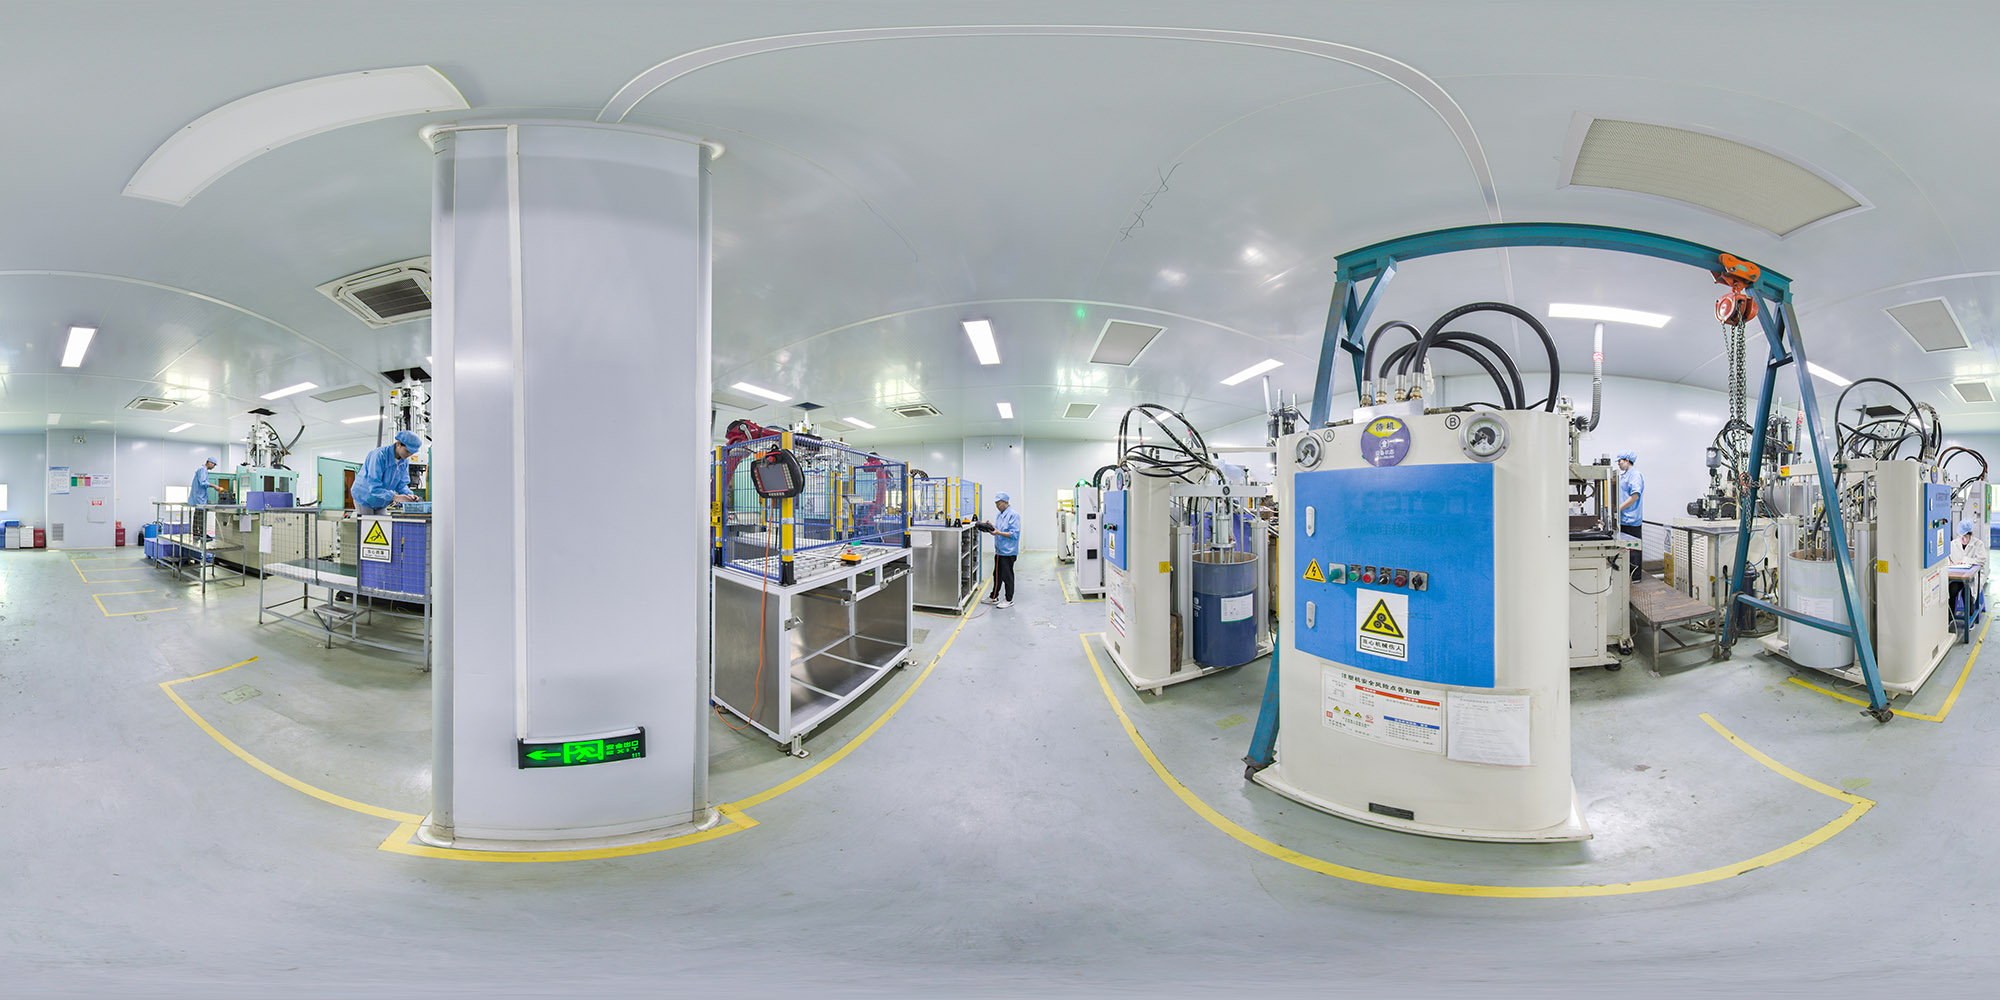
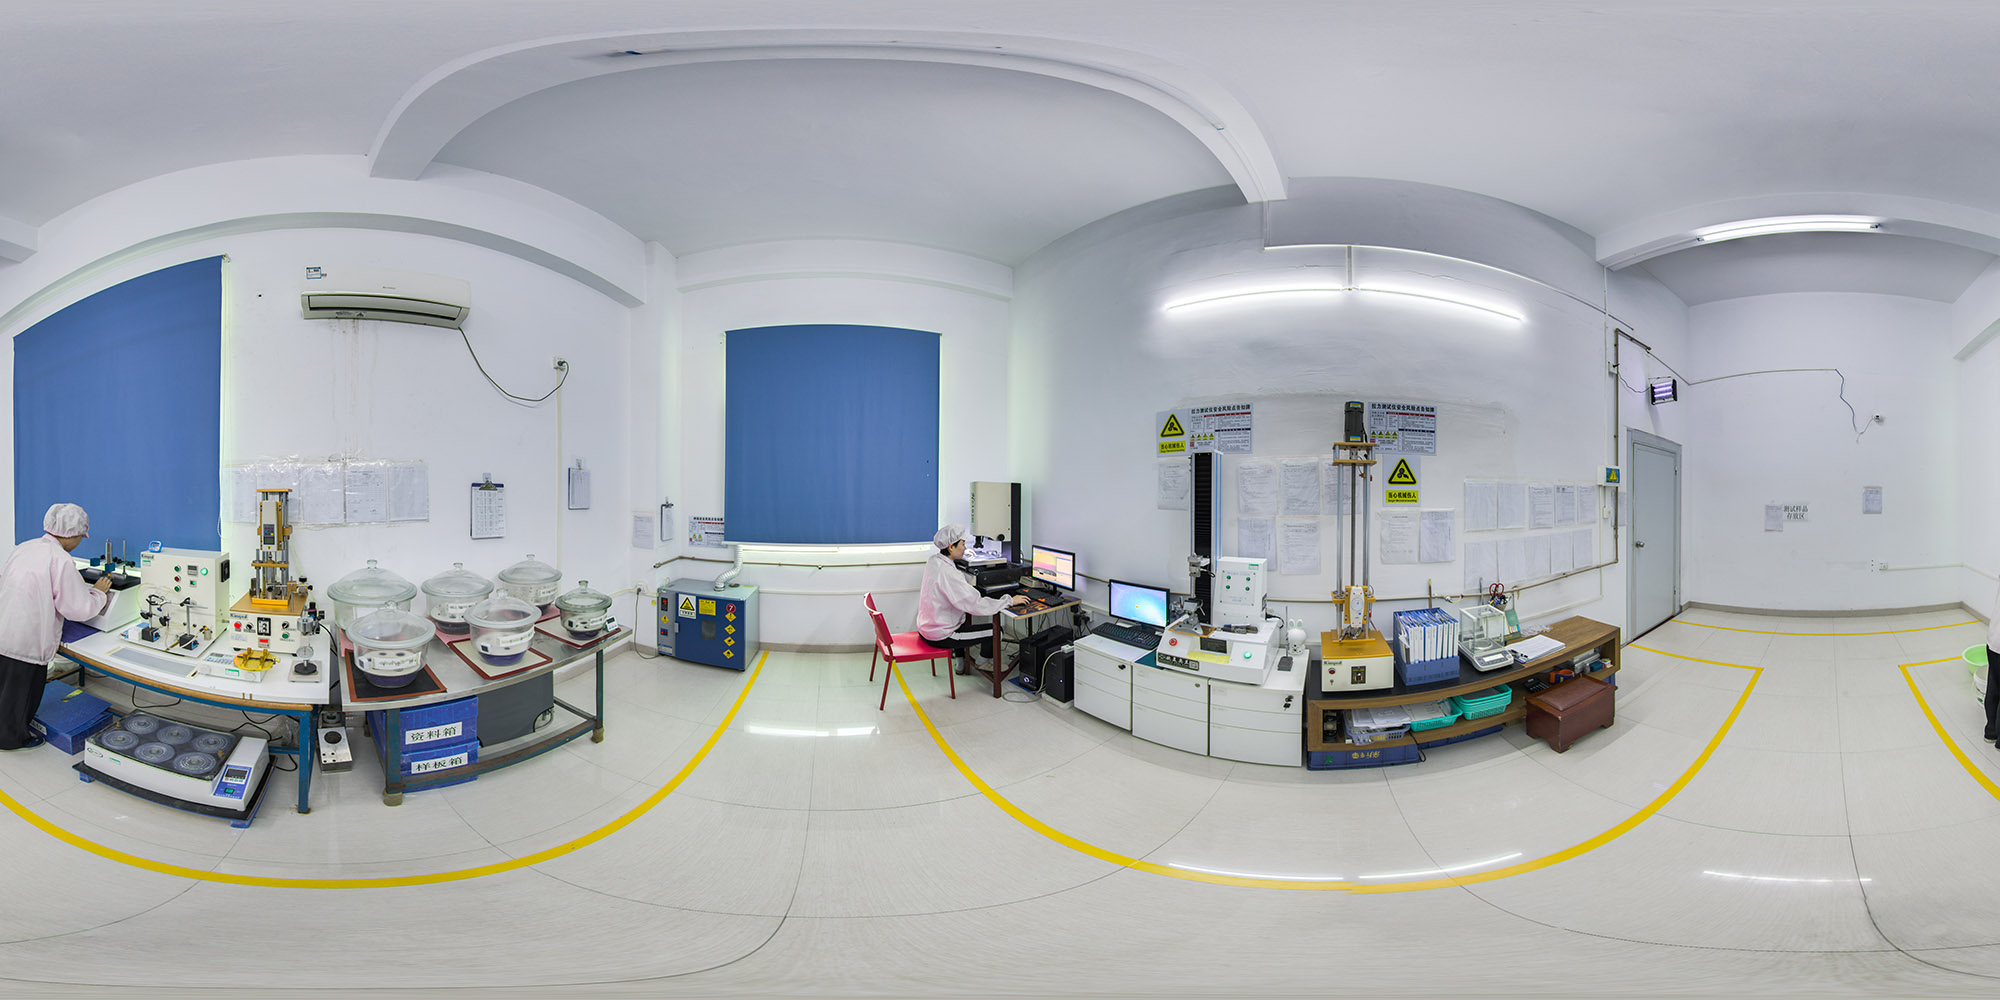
We adhere to international quality standards and hold certifications including ISO 9001: 2015, ISO 13485 FDA, LFGB, and RoHS. Our manufacturing processes are regularly audited to ensure compliance with safety and environmental regulations. We place utmost importance on protecting clients' intellectual property and proprietary information, implementing strict confidentiality protocols throughout every project phase.
Partnering with an experienced custom silicone manufacturer ensures your medical devices meet strict quality metrics and functional demands.
20 years of focused experience in silicone product manufacturing.
Advanced LSR/HTV molding and multi-material overmolding capabilities.
Certified production with rigorous quality control systems.
Secure handling of client designs and business information.
Dedicated to delivering tailored solutions, on-time delivery, and exceptional support.
Looking ahead, Kingod aims to further innovate in eco-friendly and high-precision silicone applications, particularly in the medical, automotive, and consumer electronics sectors. We are expanding our R&D team and automation capabilities to enhance efficiency and product versatility. Our vision is to become a globally recognized silicone solutions provider, driven by technology, sustainability, and customer-centric values.
As the healthcare industry shifts toward personalized medicine and home-based patient care, the demand for customizable, user-friendly, and highly durable medical silicone containers will continue to expand. Kingod is committed to investing in cleanroom facilities, advanced liquid injection molding machinery, and automated optical inspection (AOI) systems to stay at the forefront of medical silicone fabrication.
Explore our full range of custom silicone products manufactured under strict quality standards for global OEM/ODM clients.